Buying industrial hard chrome plating is not simply a search for the lowest price. It is a decision about wear resistance, dimensional control, adhesion, and long-term equipment reliability. A bright surface can look impressive under workshop lights. It can still fail early if the base metal was poorly prepared or the deposit lacks uniform thickness. The right supplier must understand your part, operating conditions, and inspection requirements.
Frank G. Altmayer, a respected electroplating educator, emphasizes this practical principle: “A coating cannot compensate for a poorly prepared surface.” That advice deserves attention. Buyers should ask how the supplier cleans, activates, masks, and pre-grinds each component. They should also request measured thickness reports, adhesion results, surface-finish data, and evidence of process control. Do not accept vague promises. Ask precise questions.
This guide introduces seven useful tips for choosing industrial hard chrome plating. It examines substrate compatibility, chrome thickness, tolerance changes, grinding capability, repair procedures, quality documentation, and supplier experience. Hydrogen-related risks may also require careful technical review, especially for high-strength steels. A responsible plater should explain the applicable controls clearly. Some buyers focus too heavily on hardness numbers. That can be a mistake. Actual service life may depend more on lubrication, geometry, counterface material, and surface finish. Every project has compromises. A cheaper quotation may reduce inspection depth, masking accuracy, or post-plating grinding quality. Those details are easy to overlook. They can become expensive later.
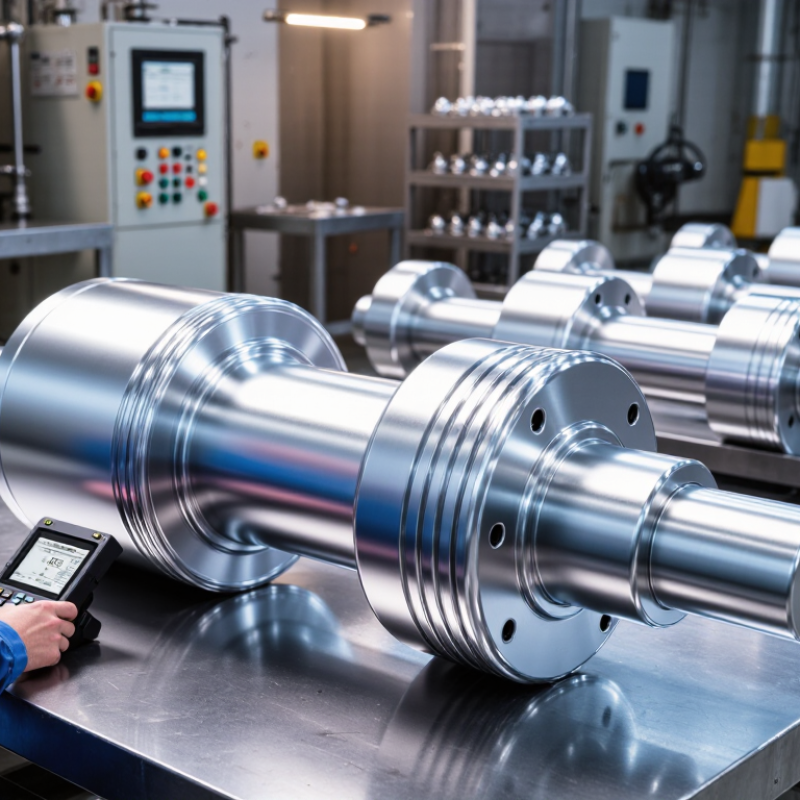
7 Tips for Buying Industrial Hard Chrome Plating
Understanding Industrial Hard Chrome Plating Requirements
Buying hard chrome plating starts with the operating conditions, not the coating price. Define load, sliding speed, temperature, lubricant, and corrosion exposure. A shaft in abrasive slurry needs different protection from a dry hydraulic rod. ASM Handbook, Volume 5A, reports typical hard chrome hardness near 800–1,000 HV. That range can vary with bath chemistry and process control.
Specify coating thickness in microns, not simply “heavy chrome.” Industrial applications commonly use about 25–250 μm, according to technical guidance from surface engineering publications. Ask whether the quoted thickness means before or after grinding. This detail changes the final dimension. Include base-metal grade, hardness, surface roughness, edge geometry, and masking areas. A drawing may look complete yet omit the grinding allowance.
Request measurable acceptance data. ASTM B650 and ISO 6158 provide useful frameworks for electrodeposited chromium coatings. Ask for thickness readings, adhesion checks, surface-finish results, and process records. For high-strength steel, require a documented hydrogen-relief procedure. It reduces embrittlement risk, although it does not eliminate every failure mode. One practical warning: hardness alone is not proof of service life. Poor preparation, sharp edges, or trapped grinding heat can still cause early peeling. I would also question unusually low prices. They may reflect missing inspection, insufficient finishing, or unrealistic tolerances.
Understanding the required deposit thickness helps buyers compare plating suppliers, control costs, and avoid premature wear. The chart shows representative engineering thickness ranges for common industrial hard chrome applications.
7 Tips for Buying Industrial Hard Chrome Plating
Evaluate the coating, not only its bright appearance. Ask for measured thickness at edges, corners, and working zones, since uneven deposits can shorten service life. Confirm adhesion through an appropriate test for the substrate and application. A cross-section inspection can reveal cracks, voids, or poor bonding that visual checks miss. Request hardness results and the test method used. Values without test conditions are difficult to compare.
Match surface roughness to the actual duty. Sealing surfaces may need a fine, controlled finish, while sliding parts require suitable texture for lubricant retention. Check roundness, straightness, and final dimensions after grinding or polishing. Even a small dimensional change can affect a hydraulic fit. Ask how porosity, edge buildup, and masking areas are controlled. These details often decide field performance.
Review sample records, inspection equipment, and traceability before placing a large order. I once focused too much on hardness and overlooked a rough sealing land; the part passed inspection but performed poorly. That mistake still matters. Require sample testing under realistic load, speed, temperature, and lubricant conditions when possible. Compare wear, friction, and corrosion results with the original specification. A flawless-looking finish can still fail early. Ask for clear acceptance limits, not vague promises.
Selecting a Qualified Hard Chrome Plating Supplier
In practical sourcing, a polished brochure means little without process evidence. Look for a supplier that understands your base material, operating temperature, load, and required coating thickness. Ask how they control grinding, masking, bath chemistry, and final dimensions. Ask for evidence. Review recent inspection reports, test methods, and material traceability records. A qualified supplier should explain results clearly, not hide behind technical language.
Tip 1: Request samples from similar components. Examine edge coverage, surface finish, hardness, and dimensional consistency. Tip 2: Confirm the supplier’s inspection equipment and calibration records. Measurements should be repeatable, especially on shafts, hydraulic parts, and sealing surfaces. Tip 3: Discuss repair procedures before production begins. Rework can change dimensions or surface integrity, and vague answers create expensive delays.
Experience also matters. Ask how the team handles pitting, uneven deposition, poor adhesion, and substrate damage. Their answer should include causes, corrective actions, and prevention. A perfect claim can still hide weak process control. I would rather see an honest limitation than an effortless promise. Check capacity, lead times, communication habits, and packaging methods. The supplier should protect finished surfaces during transport and provide clear acceptance criteria. Small details matter. A reliable partner welcomes technical questions and records every critical step.
| Tip | Selection Dimension | What to Confirm | Objective Evidence to Request | Practical Evaluation Rule |
|---|---|---|---|---|
| 1 | Verify relevant process experience | Confirm that the supplier regularly plates the same base materials, part sizes, geometries, and service conditions as your components. |
|
Choose a supplier that can demonstrate repeatable results on comparable parts rather than relying only on general plating capacity. |
| 2 | Define coating requirements before comparing quotations | The purchase specification should identify the required coating thickness, finished dimensions, surface finish, hardness, adhesion, coverage, and allowable defects. |
|
Reject quotes that use only a generic description such as “hard chrome finish” without measurable acceptance criteria. |
| 3 | Check standards and test-method control | Ensure the supplier can work to the applicable customer specification and recognized methods for electrodeposited chromium coatings. |
|
Standards should be selected according to the part and application; a standard reference alone does not replace project-specific requirements. |
| 4 | Evaluate measurement and inspection capability | Confirm that inspection equipment can measure the actual coating characteristics at the required locations and tolerances. |
|
Prefer suppliers that provide traceable, batch-specific inspection data rather than a simple pass/fail statement. |
| 5 | Assess substrate preparation and hydrogen-management controls | Hard chrome performance depends strongly on cleaning, activation, grinding, stress control, and the condition of the substrate. High-strength steels may require special hydrogen-embrittlement controls. |
|
Do not approve a supplier solely on final appearance; require evidence that substrate and post-treatment risks are controlled. |
| 6 | Review capacity, lead time, and process repeatability | Verify that the supplier can handle the part envelope, batch size, production schedule, repair frequency, and required consistency. |
|
A supplier should explain how it will maintain coating thickness, finish, and dimensions across the full batch—not only on a first article. |
| 7 | Compare total cost, quality risk, and communication | The lowest unit price may not be the lowest total cost if it excludes grinding, masking, inspection, stripping, rework, packaging, or freight. |
|
Select the supplier offering the best documented balance of technical compliance, repeatability, delivery reliability, and total lifecycle cost. |
Important: Coating thickness, hardness, surface finish, dimensional allowance, post-treatment, and inspection methods must be established from the component material, geometry, operating environment, and applicable engineering specification. Typical values should not be adopted without application-specific validation.
Price should never stand alone. Grand View Research valued the global electroplating market at about USD 18.9 billion in 2023, with continued growth forecast through 2030. That demand can tighten capacity for large shafts, hydraulic rods, and repair work. Ask for a line-item quote covering stripping, masking, grinding, plating thickness, inspection, and final polishing. A low initial price may exclude diameter correction or post-plating grinding.
Lead time depends on geometry, not only workload. A 1.5-meter hydraulic rod may require several setup changes, while a small batch of identical sleeves can move faster. Request typical and worst-case delivery windows. ASTM B650 provides guidance for electrodeposited engineering chromium, but it does not guarantee a supplier’s schedule. Get the schedule in writing. Then test it with one pilot order.
Production capability needs measurable evidence. Check maximum part length, tank dimensions, current capacity, thickness tolerance, hardness testing, and surface-finish equipment. ISO 9001 certification supports process control, but it cannot replace recent inspection records. Ask for sample certificates and coating-thickness maps. The U.S. Department of Energy reports that industrial energy assessments often identify significant efficiency opportunities, so energy-intensive plating costs may vary sharply between facilities. I would compare at least three qualified suppliers. I would also leave room for uncertainty; promised capacity can change after an unexpected rush order.
Before buying, request a written inspection standard, not a verbal promise. It should define coating thickness, hardness, adhesion, surface roughness, and dimensional tolerance. Ask how measurements are taken and where samples are tested. A coating may look bright yet fail after limited service. Confirm the test method, inspection frequency, and acceptance limits. Require inspection records linked to each part or batch. Traceability matters when a cylinder later develops scoring.
Maintenance requirements should be practical for your operating environment. Ask whether the surface needs polishing, cleaning, lubrication, or scheduled wear checks. Fine dust can act like sandpaper inside seals. Record leakage, friction changes, and visible lines during routine inspections. Rework limits should be written clearly. Rework matters.
Long-term support often reveals the real supplier quality. Check whether technical drawings, coating data, and repair instructions remain available after delivery. Ask about response times for defects and whether failure analysis includes photographs, measurements, and root-cause findings. Replacement tooling and repeat-order consistency also deserve attention. Do not choose solely by the lowest quotation. I have seen purchasing teams overlook support details, then struggle when an old component needs matching dimensions. A trial order can expose weaknesses before production expands. Still, even a successful trial does not guarantee perfect long-term performance. Review the process again after several service cycles.