Chrome plating is not one uniform finish. It is a family of engineered surface treatments, each suited to different performance demands.
Dr. N. V. Parthasaradhy, a respected electroplating author and educator, described electrodeposition as “both a science and an art.” That observation still matters. A mirror-like bumper, a hard hydraulic rod, and a dark decorative trim may all appear chrome-plated. Their preparation, coating structure, thickness, and testing requirements can differ considerably.
This guide examines the top 10 types of chrome plating, including decorative chrome, hard chrome, micro-thin chrome, black chrome, and trivalent chrome. It also considers satin finishes and specialized plating systems used for wear resistance, corrosion control, appearance, or dimensional recovery. The details matter. A poorly cleaned steel part may show blistering near an edge. An improperly controlled bath can produce dull patches, pits, or uneven thickness around corners.
The list is practical, not absolute. “Top” depends on the component, service environment, budget, and required finish. That deserves honest attention. Some older processes remain technically effective, while newer alternatives may offer easier compliance and safer plant management. Specifications and regulations can also change.
The aim is clarity. Each section connects coating type with real applications, measurable benefits, limitations, and inspection considerations. Readers should still confirm material compatibility and current regional requirements with a qualified plating professional. A polished surface is only the beginning. Performance is the real test.
Chrome plating is an electrochemical coating process. It deposits chromium onto a prepared metal surface. The result depends on thickness, surface preparation, chemistry, and finishing conditions. Chrome is not simply a shiny outer skin. It forms part of a layered structure.
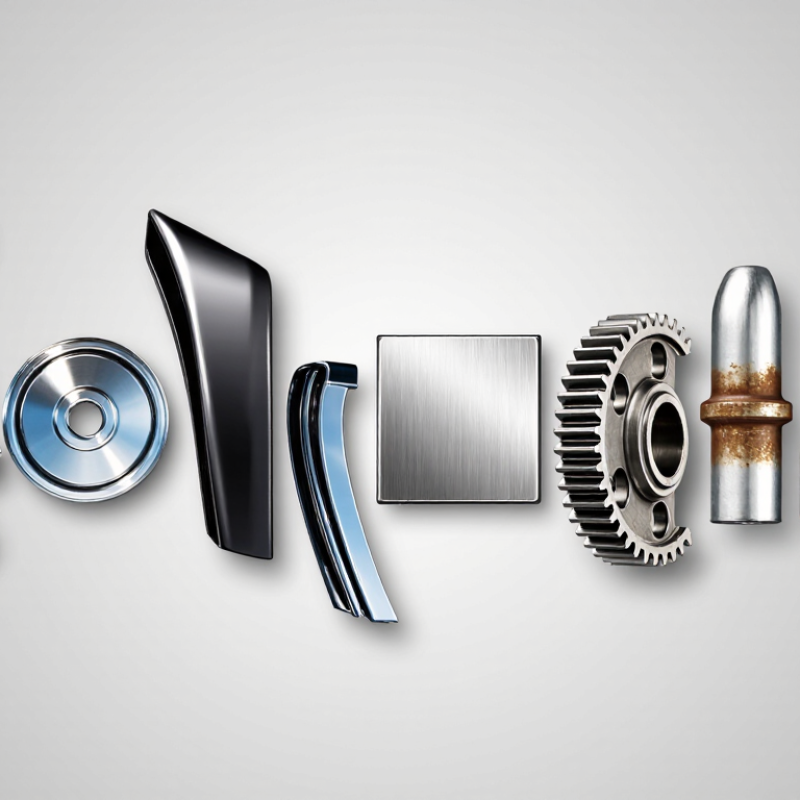
A typical decorative system contains a substrate, a nickel layer, and a thin chromium layer. Hard chrome usually deposits directly onto steel or another engineered substrate. The ten common classifications are decorative bright chrome, satin chrome, matte chrome, black chrome, hard chrome, microhard chrome, porous chrome, cracked chrome, thin dense chrome, and trivalent chrome. These names describe appearance, performance, surface texture, or process chemistry. The boundary is not always clean.
Decorative bright chrome is chosen for visual brightness and corrosion support. Satin and matte finishes reduce glare and create a softer texture. Black chrome uses controlled chemistry and requires careful color inspection. Hard chrome supports wear resistance and dimensional repair. Microhard chrome suits precision parts with tighter thickness control. Porous and cracked finishes can retain lubricants on sliding components. Thin dense chrome offers a compact protective layer. Trivalent chrome refers to the chromium chemistry, not necessarily the final appearance. That distinction is often missed.
Practical inspection should check adhesion, thickness, pores, cracks, edge coverage, and substrate damage. A polished panel may look excellent while hiding weak preparation underneath. Classification helps, but it never replaces testing.
Chrome plating is not one uniform finish. The ten main types differ in thickness, appearance, chemistry, and service purpose.
In practical inspection, the best choice starts with the component’s base metal, tolerance, load, and environment. I have seen attractive decorative work fail when edges were poorly prepared. Hard chrome can also distort a tight fit if thickness is overlooked.
Micrometers, adhesion checks, and corrosion testing reveal problems that visual inspection misses. The boundary between “porous” and “micro-porous” is not always described consistently, which deserves caution.
Ask for measurable specifications. A reliable plating plan identifies coating thickness, surface roughness, masking limits, and post-treatment requirements before production. Small details matter.
Decorative chrome plating combines visual appeal with protection against moisture, fingerprints, and surface wear. The finish usually depends on the base metal, nickel layers, and final chromium deposit.
Other useful types include smoked chrome, pearl chrome, microcracked chrome, microporous chrome, and trivalent decorative chrome.
Smoked chrome gives silver a gray tint. Pearl chrome scatters light for a softer appearance.
Microcracked and microporous finishes can improve corrosion resistance by reducing localized attack through the chromium layer. Trivalent chrome describes a plating process rather than a simple color, and it can support modern production requirements when properly controlled.
In practical inspection, I look for even color, clean edges, and consistent reflection. Tiny pits often become visible under bright workshop lighting.
A perfect mirror finish is not always the best choice. Satin surfaces may perform better in high-touch areas because they conceal minor marks.
Still, appearance can change when cleaning is too abrasive or the nickel layer is uneven. Plating thickness, surface preparation, and sealing details deserve equal attention.
The finish is only as reliable as the layers beneath it.
What Are the Top 10 Types of Chrome Plating?
Chrome plating is not one universal finish. The top ten types commonly include decorative chrome, hard chrome, micro-cracked chrome, porous chrome, crack-free chrome, thin dense chrome, flash chrome, black chrome, engineered chrome, and lubricated chrome. For industrial protection, hard chrome remains especially valuable. It creates a tough surface that reduces wear, friction, scoring, and repeated sliding damage.
Hard chrome can be tailored for shafts, hydraulic rods, molds, rollers, and forming tools. Micro-cracked and porous structures can retain oil, helping components move with less friction. Crack-free chrome may resist certain corrosive environments more effectively, but it is not automatically the best choice. Coating thickness, base material, surface preparation, hardness, and operating temperature all affect performance. A smooth shaft may need a different deposit than a rough, heavily loaded roller. Inspection should include thickness testing, adhesion checks, surface roughness, and dimensional verification. Poor preparation can ruin an excellent plating specification.
Tips: Define the failure first. Is it abrasion, galling, friction, or corrosion? Match the chrome structure to that problem. Confirm final dimensions after grinding and polishing. Also review post-plating treatment with a qualified specialist, especially for high-strength steel parts. A practical lesson is easy to overlook: harder is not always better. Excessive hardness or thickness can cause cracking, poor adhesion, or premature failure. Test a representative part when service conditions are uncertain.
| No. | Chrome Plating Type | Typical Deposit Thickness | Typical Hardness | Primary Performance Characteristics | Common Industrial Applications | Best Use Case and Limitations |
|---|---|---|---|---|---|---|
| 1 | Conventional Hard Chrome | 25–250 μm | 800–1,100 HV | High surface hardness, good abrasion resistance, low friction, and improved resistance to mild corrosion. | Hydraulic rods, shafts, dies, rollers, molds, machine components, and general wear surfaces. | A versatile general-purpose coating. The deposit commonly contains surface microcracks, so sealing or additional protection may be required in aggressive corrosive environments. |
| 2 | Microcracked Hard Chrome | 25–250 μm | 800–1,100 HV | Controlled fine crack network distributes stress and can reduce the width of individual corrosion paths. | Hydraulic cylinders, piston rods, printing rolls, forming tools, and components exposed to repeated sliding contact. | Useful where wear resistance and improved corrosion performance are both required. Crack structure and coating quality depend strongly on process control and substrate preparation. |
| 3 | Microporous Hard Chrome | 25–150 μm | 800–1,100 HV | Numerous small pores reduce the effective cathodic area and help limit localized corrosion propagation. | Automotive and hydraulic components, precision shafts, cylinders, and parts requiring enhanced corrosion resistance. | Provides a more uniform pore structure than conventional chrome. The coating still requires suitable base-metal quality and may need a sealer for severe environments. |
| 4 | Porous Hard Chrome | 25–200 μm | 800–1,050 HV | Engineered pores retain lubricants, improve oil distribution, and reduce scuffing during sliding or reciprocating motion. | Engine cylinders, piston rings, hydraulic seals, pump parts, and high-speed sliding components. | Preferred for lubricated systems. Excessive porosity can reduce corrosion protection if the component is poorly lubricated or exposed to corrosive fluids. |
| 5 | Crack-Free Hard Chrome | 10–100 μm | 850–1,100 HV | Low-crack or crack-free structure improves barrier protection and can reduce pathways for corrosive attack. | Precision tooling, sealing surfaces, hydraulic equipment, and parts where corrosion resistance is more important than oil retention. | Suitable for applications requiring a dense barrier layer. It may require specialized plating chemistry and careful control of internal stress. |
| 6 | Thin Dense Hard Chrome | 5–25 μm | 800–1,050 HV | Low dimensional change with a hard, dense surface and relatively low coating build-up. | Precision valves, seals, small shafts, bearing surfaces, and components with tight dimensional tolerances. | Ideal when post-plating machining is limited. It provides less wear-life reserve than a thicker coating and is not intended for major dimensional restoration. |
| 7 | Thick-Build Hard Chrome | 100–500+ μm | 750–1,050 HV | Restores worn dimensions and provides a substantial wear allowance for subsequent grinding or polishing. | Large hydraulic rods, worn shafts, rolls, landing-gear components, heavy machinery parts, and repair applications. | Best for dimensional recovery and long service life. Thick deposits require stress control, adequate edge preparation, and precision finishing. |
| 8 | Engineered-Profile Hard Chrome | 25–150 μm | 800–1,100 HV | Surface texture is intentionally controlled to balance friction, lubricant retention, sealing, and wear behavior. | Sealing lands, sliding guides, hydraulic components, rolls, and precision wear interfaces. | Useful when surface roughness and bearing-area ratio are critical. Final performance depends on grinding, honing, polishing, and the mating material. |
| 9 | Black Hard Chrome | 10–75 μm | 600–900 HV | Dark appearance, low reflectivity, moderate wear resistance, and useful resistance to glare and mild corrosion. | Optical and imaging equipment, military hardware, instruments, decorative-functional parts, and components requiring a non-reflective finish. | Chosen mainly for appearance and low reflectivity rather than maximum abrasion resistance. It is generally less hard and less wear-resistant than bright hard chrome. |
| 10 | Low-Temperature Hard Chrome | 25–250 μm | 800–1,100 HV | Deposited under controlled lower-temperature conditions to help reduce thermal effects on heat-sensitive substrates and assemblies. | Precision tools, hardened steels, repaired components, assemblies with tight dimensional requirements, and parts sensitive to heat treatment changes. | Helpful when substrate distortion or metallurgical alteration must be minimized. Required process parameters vary with the substrate, geometry, and coating specification. |
| Typical values are engineering ranges rather than guaranteed specifications. Actual hardness, thickness, porosity, crack density, friction, and corrosion performance depend on the substrate, plating chemistry, current density, temperature, surface preparation, finishing method, and service environment. | ||||||
Selecting chrome plating begins with the working environment, not appearance. The ten common choices include decorative chrome, hard chrome, microcracked chrome, microporous chrome, porous chrome, black chrome, trivalent chrome, hexavalent chrome, thin dense chrome, and engineered chrome. Each behaves differently under friction, moisture, heat, and chemical exposure.
Decorative chrome suits handles, fittings, and visible components. Its bright surface is usually thin, so it needs a durable nickel foundation. Hard chrome is better for shafts, hydraulic rods, and molds facing repeated wear. Typical hard-chrome thickness ranges from 25 to 500 micrometres, depending on load and finishing requirements. Microcracked and microporous finishes help distribute corrosion sites across the surface. Choose them for outdoor parts where appearance and protection must coexist. Porous chrome can retain lubricants on sliding surfaces. That sounds useful. It can also trap contaminants.
Black chrome works when low reflectivity matters, but its darker appearance may hide early surface damage. Trivalent chrome can reduce certain process hazards, while hexavalent chemistry requires strict engineering controls and regulatory review. Thin dense chrome fits precision parts where dimensional change must remain small. Engineered chrome should be specified only after testing temperature, load, and lubricant compatibility.
The IMPACT corrosion study estimated global corrosion costs at about 3.4% of worldwide economic output. That figure supports lifecycle thinking, not automatic overcoating. Compare salt-spray results, hardness, thickness tolerance, and repairability. ASTM B456 and ISO 6158 provide useful specification frameworks. Still, laboratory results may not match a dusty factory or coastal road. Test representative parts. Mistakes often begin with choosing chrome by color alone.
Chrome plating types are selected according to appearance, corrosion resistance, friction, wear, and dimensional requirements. The chart compares industry-typical coating thickness ranges; actual values vary with the substrate, process specification, and application.
Decorative chrome is generally thin and is used mainly for appearance and corrosion protection. Hard chrome is substantially thicker and is commonly selected for wear resistance, low friction, and dimensional restoration. Porous and microcracked structures can help retain lubricants or improve corrosion performance when correctly specified.