How to Choose Black Chrome Electroplating Suppliers?
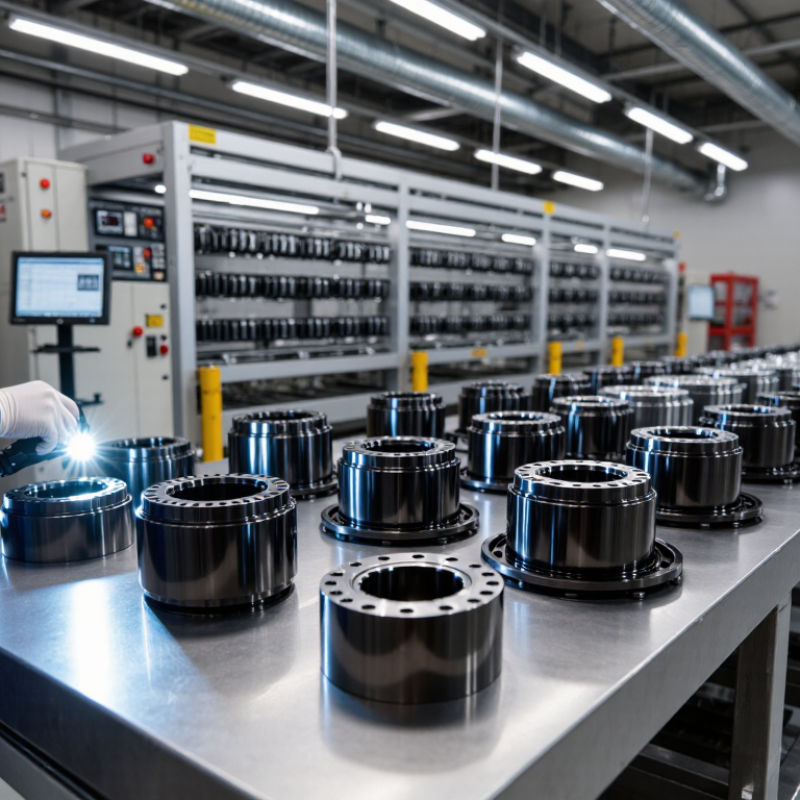
Choosing a black chrome electroplating supplier requires more than comparing prices and sample colors. The finish should match your product’s purpose, surface material, and expected service environment. A decorative component may need a deep, uniform appearance, while an automotive or industrial part may require stronger wear resistance. Small details matter. Inspect edges, corners, rack marks, and recessed areas under bright lighting.
An experienced supplier should explain each process stage clearly, including cleaning, activation, plating thickness, sealing, and final inspection. Ask how the company tests adhesion, corrosion resistance, color consistency, and surface hardness. Request recent test records, not only attractive samples. Salt-spray results can be useful, but they should reflect your actual application. A reliable supplier will also discuss substrate limitations and possible defects before production begins.
Certification can support trust, but it does not replace direct evaluation. Review quality systems, equipment maintenance, environmental controls, and production capacity. Confirm whether the supplier can maintain stable results across small trial batches and larger orders. Communication matters too. Delayed replies may signal future problems. We have seen promising finishes fail because specifications were vague. No supplier is perfect. Even strong manufacturers may face variation between materials or batches. The right partner acknowledges these risks and proposes practical controls. Choose a supplier that provides traceable records, realistic lead times, and clear corrective actions. This approach supports consistent black chrome electroplating results and reduces costly surprises after delivery.
Define Black Chrome Specifications: ISO 1456, 0.1–1.0 μm, Color, and Wear
Choosing a black chrome electroplating supplier begins with a precise specification. ISO 1456:2009 provides a useful framework for nickel-chromium decorative and protective coatings. However, black chrome may require additional appearance controls. Ask whether the stated 0.1–1.0 μm applies to the black chromium layer or the complete chromium system. This detail is often missed. It can change performance expectations.
Require thickness results from X-ray fluorescence testing under ASTM B568. The report should show measurement locations, average values, minimum readings, and instrument uncertainty. One polished panel is not enough. Request readings from edges, recesses, and functional surfaces. Color should use CIELAB values, gloss, lighting conditions, and an agreed color difference limit. ASTM D2244 supports color-difference evaluation, while ASTM D523 can define gloss measurement. A visual sample alone is weak evidence.
Wear performance needs a stated method, load, counterface, cycle count, and failure criterion. ASTM B611 offers a recognized abrasive-wear method for metallic coatings, but it may not represent every service environment. Ask for actual test records, not only a certificate. ISO 1456 compliance also does not automatically prove long-term black color stability. Humidity, handling, and substrate preparation can affect results. Supplier experience matters here, yet experience should be documented with process records and repeat-test data. A reasonable qualification plan includes three production samples, independent inspection, and a written agreement on acceptable color variation. Even then, the specification may need revision after field exposure.
Verify Coating Performance with ASTM B117 Salt-Spray and Adhesion Tests
How to Choose Black Chrome Electroplating Suppliers?
Black chrome looks refined, but appearance cannot prove coating durability. The AMPP/NACE IMPACT Study estimated annual corrosion costs at about 3.4% of global GDP. That figure makes supplier verification practical, not decorative. Ask for recent laboratory records, coating thickness readings, pretreatment details, and complete failure photographs.
Request ASTM B117 salt-spray testing under controlled conditions. The method commonly uses a 5% sodium chloride solution, around 35°C, with defined spray collection rates. Do not judge suppliers by hours alone. ASTM B117 creates comparative exposure, but it does not predict outdoor service life. Specify the test duration, substrate, edge protection, and acceptable red-rust area before testing begins. Small differences matter.
Then require an adhesion test, such as ASTM D3359 crosshatch evaluation. A 5B rating shows no coating removal in the tested grid, while lower ratings reveal progressive failure. Test both flat surfaces and sharp edges. Real components rarely behave like perfect laboratory panels. That is the uncomfortable part. I have seen visually excellent finishes fail after poor cleaning, even when thickness appeared acceptable. Require batch traceability, calibrated instruments, and independent retesting when results conflict. A supplier who explains limitations is usually more reliable than one promising unlimited salt-spray hours.
Audit RoHS and REACH Controls for Hexavalent Chromium Restrictions
How to Choose Black Chrome Electroplating Suppliers?
A reliable black chrome supplier should show more than a polished sample. Ask for the plating process flow, chemical inventory, bath-control records, and recent laboratory reports. Hexavalent chromium can appear during processing, even when the finished surface looks uniform and dark. Under RoHS, chromium VI is restricted to 0.1% in each homogeneous material. Test reports should identify the sample location, preparation method, detection limit, and laboratory accreditation. EN 15205 can support hexavalent chromium analysis in surface coatings, while IEC 62321 methods may apply to relevant electronic materials.
REACH requires a separate review. Check whether any chromium VI compound is listed under Annex XVII or the Candidate List, and confirm the supplier’s duty to communicate substances above 0.1% in articles. Do not accept a generic “REACH compliant” letter. Request the exact substance assessment, safety data, supplier declaration, and change-notification procedure. ECHA’s enforcement reporting has repeatedly found chemical-law failures in inspected products; its recent project identified non-compliance in about 18% of checked products. That figure should make procurement teams uncomfortable.
Audit the factory, if possible. Look for labeled process tanks, closed wastewater lines, calibrated meters, and dated bath logs. Review worker-protection controls too. A complete file can still hide weak production discipline. I would sample finished parts from different lots, not only the best-looking batch. Recheck after process changes, because “chromium-free” claims sometimes describe the final coating, not the entire manufacturing route.
Hexavalent Chromium Controls for Black Chrome Plating Suppliers
Audit supplier processes against the limit that applies to the final product and its intended use. RoHS restricts hexavalent chromium to 0.1% by weight, equivalent to 1,000 mg/kg, in each homogeneous material of covered electrical and electronic equipment. REACH sets more specific limits for certain uses, including 2 mg/kg of soluble chromium(VI) in hydrated cement and 3 mg/kg in leather articles that contact skin.
A black chrome supplier should provide material declarations, coating-process controls, test reports, corrective-action records, and evidence that chromium(VI) is not introduced or left above the applicable limit.
Compare Suppliers by ISO 9001 Systems, Yield Rates, Lead Times, and Cost per Part
Choosing a black chrome electroplating supplier requires more than comparing quoted prices. A reliable evaluation begins with the supplier’s ISO 9001 quality system. Ask for current certification, process procedures, inspection records, and corrective-action examples. A certificate alone proves little. The daily records matter more.
Yield rate shows how consistently the supplier converts production lots into acceptable parts. Request yield data from recent, similar components, not only annual averages. Check rejection causes, rework frequency, coating thickness, color variation, and adhesion results. For example, a 96% first-pass yield may outperform a cheaper supplier reporting 88%. Still, figures can be selective. Review sample inspection sheets and, when possible, observe a production run.
Lead time should include scheduling, pretreatment, plating, inspection, and packaging. Confirm realistic capacity during peak periods. A promised seven-day cycle means little if queue time adds two weeks. Compare cost per part using the same assumptions. Include tooling, setup, testing, packaging, freight, and expected scrap. A low unit price can become expensive after rework. Ask for a written cost model.
Small trials are valuable. Send production-representative parts and measure the results independently. I would also record response speed and technical clarity. A supplier that admits process limits may be safer than one offering perfect numbers. My assessment would remain provisional until three repeat lots meet the agreed standards. That caution can feel slow, but it often prevents costly surprises.
How to Choose Black Chrome Electroplating Suppliers? — Compare Suppliers by ISO 9001 Systems, Yield Rates, Lead Times, and Cost per Part
| Supplier Profile |
ISO 9001 Quality System |
First-Pass Yield |
Plating Thickness Control |
Typical Lead Time |
Tooling or Setup Lead Time |
Estimated Cost per Part |
Minimum Order Quantity |
Process Capability |
Best Fit |
| Supplier A |
Certified
Current certificate and documented corrective-action process |
98.4% |
±2.0 µm on controlled production lots |
7–10 business days |
3–5 business days |
$0.42–$0.58 |
500 parts |
Rack and barrel plating; masking and selective plating available |
High-volume parts requiring consistent cosmetic quality |
| Supplier B |
Certified
Controlled work instructions, inspection records, and supplier audits |
97.1% |
±2.5 µm on production lots |
10–14 business days |
5–7 business days |
$0.31–$0.46 |
1,000 parts |
Barrel plating for small parts; rack plating for visible components |
Cost-sensitive repeat production |
| Supplier C |
In Progress
Documented quality procedures; certification audit scheduled |
94.8% |
±3.0 µm on production lots |
8–12 business days |
4–6 business days |
$0.36–$0.52 |
300 parts |
Flexible rack plating; prototype and low-volume support |
Shorter runs and engineering validation builds |
| Supplier D |
Certified
Electronic batch traceability and formal nonconformance control |
99.0% |
±1.5 µm on qualified production lots |
12–16 business days |
6–8 business days |
$0.55–$0.78 |
750 parts |
Rack plating, tight masking, salt-spray testing, and appearance inspection |
Safety-critical or highly visible components |
| Supplier E |
Not Certified
Basic inspection checklist and manual batch records |
91.6% |
±4.0 µm on production lots |
5–8 business days |
2–4 business days |
$0.24–$0.38 |
100 parts |
General-purpose rack plating; limited process validation |
Samples, prototypes, and non-critical decorative parts |
Cost estimates are shown in U.S. dollars per part for a typical small-to-medium metal component and exclude freight, taxes, special masking, testing, and one-time tooling. Yield means the percentage of parts accepted without stripping, replating, or rework. Actual results depend on part geometry, substrate, surface preparation, black chrome specification, order volume, inspection criteria, and required corrosion resistance.